- Home
- Industries
- Aluminum Forging Vehicle Parts
- Vehicle Parts A-10
Vehicle Parts A-10
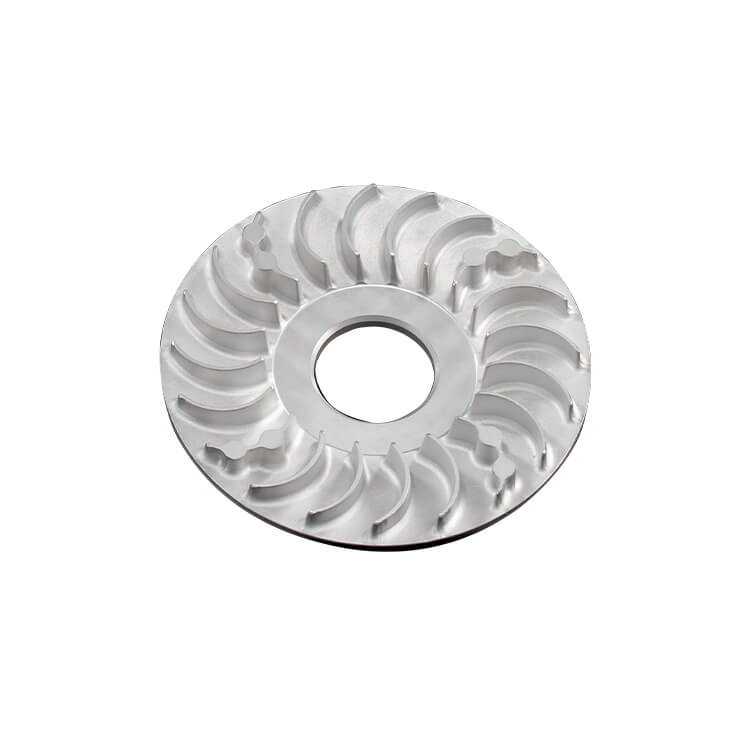
Forged Aluminum CVT Clutch Part A-10: CVT Sheave with Cooling Fins
Forged aluminum CVT clutch part A-10 is a clutch sheave for a continuously variable transmission (CVT). It is a disc with a central bore and multiple curved cooling fins arranged radially on its face. Friction between belt and sheave generates heat in operation, and the rotating fins move air to help cool the clutch and belt.
With many thin radial fins, Al Forge Tech (AFT) closed-die hot forges the fin profile directly so grain flow extends into every fin, giving a denser structure than a cast sheave and making balance easier to control. After T6 heat treatment, the center bore, face and mating surfaces are turned and CNC-machined. AFT has produced CVT transmission components for 1000cc four-wheel-drive ATVs.
Key Features
- Radial curved cooling fins forged in one operation
- Dense forged structure helps balance control of rotating parts
- Center bore, face and mating surfaces turned and CNC-machined
- Experience with CVT components for 1000cc 4WD ATVs
Forged Aluminum CVT Clutch Part A-10 Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Vehicle Parts |
| Product No. | A-10 |
| Application | CVT clutches and drivetrains for ATVs, UTVs and scooters |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Reference work | CVT transmission components for 1000cc four-wheel-drive ATVs |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum CVT Clutch Part A-10 Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
Why forge the cooling fins of a CVT sheave?
The fins are thin and numerous; machining them takes long tool paths and is prone to chatter. Casting can form them, but internal porosity may affect balance and strength at high speed. Forging forms fins and disc together with a dense structure, and fin thickness is controlled by the die for consistency, leaving only mating surfaces to finish.
How is balance controlled on a high-speed CVT part?
Imbalance in rotating parts comes mainly from uneven mass distribution and dimensional variation. AFT's dies keep fin thickness and position consistent, the dense forged structure reduces mass variation from internal defects, and the bore and face are finish-turned, with runout and flatness measured on CMM. If the drawing specifies dynamic balance, the inspection method can be discussed at quotation.
Can Al Forge Tech supply the Forged Aluminum CVT Clutch Part A-10 from forging through machining?
Yes. Forging, heat treatment, CNC machining, surface finishing and inspection are integrated in one facility: 52 CNC machining centers (40 four-axis and 12 4.5-axis), 30 lathes (14 with robotic loading), plus broaching, burnishing and centerless grinding. The Forged Aluminum CVT Clutch Part A-10 can be delivered as a forged blank, semi-finished or fully machined part.
Can you assess forging feasibility while the Forged Aluminum CVT Clutch Part A-10 is still in design?
Yes. Al Forge Tech works mainly as an OEM supplier, and our engineers can give design-for-manufacturability (DFM) feedback at the concept or drawing stage, such as adjusting thin ribs, abrupt section changes or draft angles to avoid laps and underfill. QForm simulation predicts metal flow early, and the results are cross-checked against our die design experience.
How do you keep the Forged Aluminum CVT Clutch Part A-10 consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum CVT Clutch Part A-10 stable across lots.
Request a Quote for the Forged Aluminum CVT Clutch Part A-10
Developing a new Forged Aluminum CVT Clutch Part A-10 or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Vehicle Parts and our automotive aluminum forging applications, or visit About Us for our equipment and certifications.