- Home
- Industries
- Aluminum Forging Vehicle Parts
- Upper Metal
Upper Metal
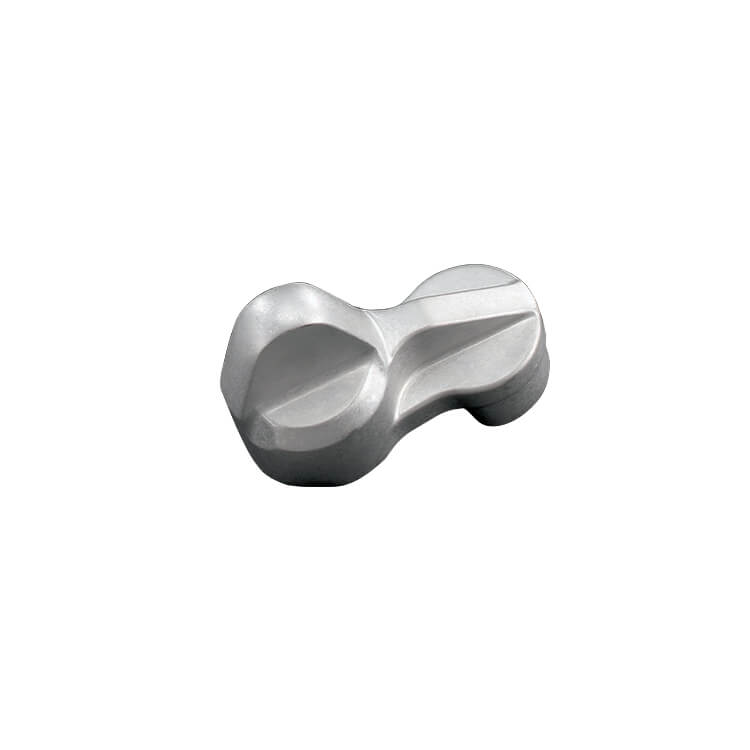
Forged Aluminum Shock Upper Mount (Double Head): One-Piece Suspension Connector
This double-head forged aluminum upper metal is a suspension connector made of a larger and a smaller round head joined by a neck. The face of the larger head has a slot that can be machined into a pin bore or clamping slot, while the smaller head connects to the shock or linkage. The compact double-head form carries reciprocating shock loads in a small space.
The neck between the heads has the largest change in section. Al Forge Tech (AFT) hot forges the part so grain flow runs continuously through both heads and the neck, avoiding a cut flow line at the neck as in machined parts. After in-house T6 heat treatment, the pin bore, slot and mating faces are CNC-machined, with anodizing available. AFT's suspension work spans automotive, motorcycle, recreational vehicle and bicycle shock systems.
Key Features
- Two heads and neck forged in one piece with continuous grain flow
- Face slot machinable as a pin bore or clamping slot
- Compact form suits tight shock mounting spaces
- T6, CNC machining and anodizing in one facility
Forged Aluminum Shock Upper Mount (Double Head) Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Vehicle Parts |
| Application | Shock absorber upper mounts, suspension linkage connectors |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Per customer specification; 6xxx alloys common for chassis and suspension parts (e.g. 6061, 6082, 6110), 7xxx evaluated for higher strength |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Shock Upper Mount (Double Head) Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
How is strength ensured at the neck of a double-head part?
The neck is where the section narrows between the two heads and where stress concentrates under load. Forging carries grain flow continuously from the large head through the neck into the small head, rather than cutting it as machining would. At the DFM stage AFT also recommends neck radii to reduce stress concentration, and T6 heat treatment raises material strength.
Can suspension parts be delivered as forged blanks for customer machining?
Yes. AFT can deliver heat-treated forged blanks, semi-finished parts or fully CNC-machined and finished parts as required. If you machine in-house, please specify machining allowances and datums on the drawing; AFT will provide matching locating datums on the forging for your downstream machining.
How does a forged aluminum Forged Aluminum Shock Upper Mount (Double Head) compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Shock Upper Mount (Double Head) under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
Can Al Forge Tech supply the Forged Aluminum Shock Upper Mount (Double Head) from forging through machining?
Yes. Forging, heat treatment, CNC machining, surface finishing and inspection are integrated in one facility: 52 CNC machining centers (40 four-axis and 12 4.5-axis), 30 lathes (14 with robotic loading), plus broaching, burnishing and centerless grinding. The Forged Aluminum Shock Upper Mount (Double Head) can be delivered as a forged blank, semi-finished or fully machined part.
How do you keep the Forged Aluminum Shock Upper Mount (Double Head) consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Shock Upper Mount (Double Head) stable across lots.
Request a Quote for the Forged Aluminum Shock Upper Mount (Double Head)
Developing a new Forged Aluminum Shock Upper Mount (Double Head) or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Vehicle Parts and our automotive aluminum forging applications, or visit About Us for our equipment and certifications.