- Home
- Industries
- Aluminum Forging Vehicle Parts
- Upper Control Arm
Upper Control Arm
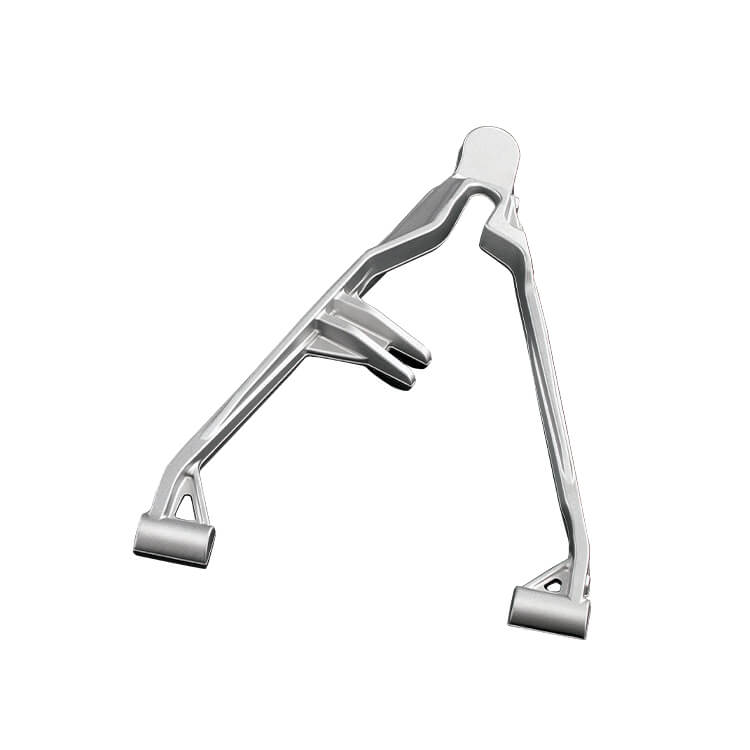
Forged Aluminum Upper Control Arm: Upper A-Arm with Integrated Shock Mount
The forged aluminum upper control arm is an upper A-arm for powersport vehicle suspension. Two slender arms meet at the apex to form the ball-joint seat, with bushing seats at each end, and one arm carries a double-ear mounting bracket at mid-length for a shock absorber or sway-bar link. Together with the lower arm, the upper arm defines the wheel's motion path.
The mid-arm double-ear bracket makes the shape more complex. Al Forge Tech (AFT) closed-die hot forges the arms, mounting ears and seats in one operation so grain flow is continuous from the ear roots into the arm, avoiding the heat effects of welded brackets. After in-house T6 heat treatment, the ball-joint seat, bushing bores and ear holes are CNC-machined and their relationships verified on CMM.
Key Features
- Arms, double-ear bracket and seats hot forged in one operation
- Integrated shock or link mounting ears, no welding
- Slender arms reduce unsprung mass
- Multi-hole CNC machining and CMM measurement
Forged Aluminum Upper Control Arm Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Vehicle Parts |
| Application | ATV, UTV and powersport vehicle front suspension |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Per customer specification; 6xxx alloys common for chassis and suspension parts (e.g. 6061, 6082, 6110), 7xxx evaluated for higher strength |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant line; tensile and fatigue testing available |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Upper Control Arm Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
How do upper and lower control arms differ in design?
The lower arm usually carries larger vertical and longitudinal loads and has a heavier section. The upper arm mainly controls camber and wheel path, with slimmer arms, and may integrate shock or sway-bar mounting ears. Alloy, section and heat treatment are designed separately for each according to the vehicle's load cases, and AFT can evaluate a complete suspension set from the drawings.
How does a forged-in mounting ear compare with a welded one?
A welded ear requires extra welding, straightening and weld inspection, and the heat-affected zone lowers local strength. A forged-in ear is formed from the same material as the arm, with continuous grain flow and no weld; its dimensions are controlled by the die, giving better production consistency and fewer assembly steps.
Can you assess forging feasibility while the Forged Aluminum Upper Control Arm is still in design?
Yes. Al Forge Tech works mainly as an OEM supplier, and our engineers can give design-for-manufacturability (DFM) feedback at the concept or drawing stage, such as adjusting thin ribs, abrupt section changes or draft angles to avoid laps and underfill. QForm simulation predicts metal flow early, and the results are cross-checked against our die design experience.
How does a forged aluminum Forged Aluminum Upper Control Arm compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Upper Control Arm under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
How are MOQ and lead time for the Forged Aluminum Upper Control Arm determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Upper Control Arm.
Request a Quote for the Forged Aluminum Upper Control Arm
Developing a new Forged Aluminum Upper Control Arm or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Vehicle Parts and our automotive aluminum forging applications, or visit About Us for our equipment and certifications.