Forging Tonnage Explained: Why the Biggest Press Isn\'t Always the Right Supplier for Your Part
Introduction
When procurement engineers shortlist forging suppliers, the tonnage figure on the capability sheet is usually the first thing they check — and often the last thing they properly interrogate. Forging tonnage selection is not simply a matter of matching your part's size to the biggest available press; it depends on whether the part's geometry can be formed in a single die impression or requires a multi-die sequence, and getting that wrong is one of the most common — and most expensive — mistakes in supplier qualification. A supplier with a 8,000-ton press is not automatically the right fit for a small, geometrically complex bracket, just as a supplier without a large press may be unable to handle a big structural forging regardless of die design. The right question isn't "how big is your press?" It's "how did you decide this part needs one die or three, and how do you know before you cut steel?"
This matters more for aluminum forgings than most buyers expect, because aluminum's solid-state forming behavior — unlike casting, which can fill a complex cavity in one pour — depends on how metal flow is staged through the die sequence.
Why Tonnage Alone Doesn't Predict Forgeability
Tonnage tells you the maximum force a press can apply — nothing more. It doesn't tell you:
- Whether your part's geometry can be filled in one die impression, or needs a blocker (preform) die stage before the finisher die
- Whether the flash design and draft angles are appropriate for the alloy and wall thickness
- Whether the die sequence has been validated by simulation before tooling is cut
A widely applied guideline in press-selection engineering is to reserve a 20–30% tonnage margin above the calculated peak forming load, to account for material property variation, die wear, and press-alignment tolerance. That margin is a starting point for sizing the press correctly for a known forming load — but it says nothing about whether that load can even be achieved in a single die stroke without defects. For parts with deep ribs, thin walls transitioning to thick bosses, or non-axisymmetric geometry, forging engineering literature on preform design is consistent on this point: a single die impression typically cannot achieve full cavity fill on complex geometries without flow defects such as folding or underfill, which is why a blocker stage is used to progressively redistribute metal before the finisher die completes the shape.
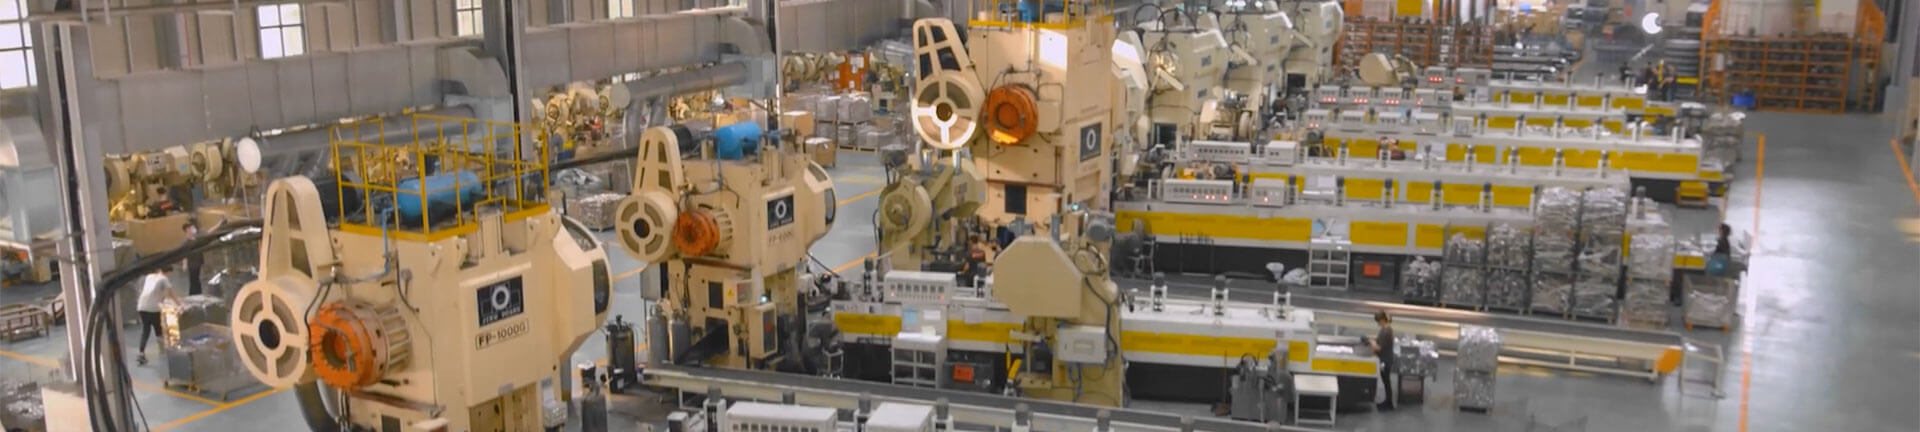
AFT operates ten forging press classes from 260 to 8,000 tons across hot and cold forging lines — including 8000T, 5000T, 4500T, dual 4000T, 3500T, 2000T, dual 1600T-plus-servo, six 1000T presses with a robotic-arm production line, and quad 600T on the hot-forging side, alongside a cold-forging line from 260T to 2500T. That range exists specifically so tonnage class and die-sequence decisions can be matched to the part rather than forced onto whichever single press a smaller supplier happens to own.
How Do You Know If a Part Needs Single-Die or Multi-Die Forging?
A part is a strong candidate for multi-die (blocker + finisher) forging rather than single-die forming when it has:
- Significant cross-sectional variation — thin walls next to thick bosses or flanges
- Deep ribs or non-symmetric branching — geometry that can't be reached by straight-line metal flow from a simple billet
- Tight grain-flow requirements for fatigue-loaded applications, where flow lines must follow the load path rather than being cut across by machining
- Multiple functional features on one forging that would otherwise require excess flash and machining stock if forced into one die
A useful reference point for complexity: forging categories such as monobloc brake calipers — parts that combine multiple mounting bosses, internal fluid channels, and structural ribs into a single forged body — commonly require a blocker die stage followed by a finisher die, and in some cases a secondary refinement pass, because solid-state metal flow cannot redistribute material the way a liquid casting process can in one shot. (Referenced here as a part-complexity category for illustration, not as a disclosed customer program.)
Single-Die vs. Multi-Die (Blocker + Finisher) Forging
| Dimension | Single-Die Forging | Multi-Die (Blocker + Finisher) Forging |
| Typical part geometry | Simple, largely axisymmetric shapes with modest cross-sectional variation | Complex geometry: deep ribs, mixed wall thickness, multiple functional features |
| Metal flow risk if mismatched | Low — flow path is short and direct | High if forced into one die: underfill, folding, or flow-line discontinuity |
| Tooling investment | Lower — one die set | Higher — blocker die + finisher die (sometimes a third refinement die) |
| Simulation validation focus | Confirm fill and flash balance | Confirm progressive volume distribution across each die stage before cutting steel |
| Grain-flow outcome | Acceptable for non-fatigue-critical parts | Preferred for fatigue-loaded, safety-critical structural parts |
| Example part class | Simple bosses, spacers, basic brackets | Monobloc calipers, control arms, multi-feature housings |
What Tonnage Margin Should You Ask a Supplier For?
Ask for the calculated peak forming load per die stage — not just the press's rated maximum. A supplier working within the standard 20–30% margin above that calculated load, on a press class matched to the part's actual required force (not simply "the biggest press we own"), is applying the same engineering logic used across the forging industry for safe, wear-appropriate operation. A press running consistently near its rated maximum accelerates die wear and increases the risk of underload defects if material properties vary batch to batch — which is exactly why matching tonnage class to the calculated load, rather than defaulting to the largest available press, is the more reliable signal of supplier competence.
AFT's forging simulation (QForm) is used to validate die-fill and volume distribution across each die stage before tooling is cut. Its predictive accuracy for solid-state aluminum forming is approximately 60–70%; the remaining variance is resolved through engineer review of die-fill risk, not left as an unaddressed gap. This is a disclosure most suppliers avoid volunteering — simulation software is a planning aid, not a guarantee, and buyers should be skeptical of any supplier claiming otherwise.
Verifying Die and Press Match During a Supplier Audit
Once a die sequence is designed and tooling is cut, the ongoing risk shifts to die wear and press alignment consistency. AFT inspects first-, mid-, and last-piece parts on every production batch, using four Zeiss coordinate measuring machines and a portable 3D scanner to compare die-cavity geometry against the original 3D model. When wear-related dimensional drift is detected, the die is routed back to die-shop refinement (die-sinking adjustment to the cavity) rather than allowed to drift into scrap — a control point that matters specifically because multi-die tooling has more cavity surfaces that can wear unevenly than a single-die setup.
The same audit-readiness logic applies downstream of forging: see how AFT controls T4/T6 heat treatment in-house for how the same first/mid/last-piece discipline extends into post-forging heat treatment.
7 Questions to Ask a Forging Supplier Before Committing Tooling Budget
- Based on my part's geometry, do you recommend single-die or multi-die (blocker + finisher) forging, and why?
- What is the calculated peak forming load per die stage, and what tonnage margin will you run at?
- What simulation software validates the die sequence, and what is its known accuracy limit for my alloy and process (hot vs. cold forging)?
- How many die stages will this part require, and what's the tooling cost difference between a two-stage and three-stage sequence?
- What in-house press tonnage range do you have, and will my part run on equipment matched to its calculated load — or on whatever press happens to be free?
- What is your first/mid/last-piece inspection method, and what equipment verifies die-cavity geometry against the original design?
- If mid-production wear variance is detected, what is your die correction process, and who owns die-shop refinement — in-house or third-party?
Frequently Asked Questions
Does a bigger press (e.g., 8,000T) mean better quality for a small, complex part?
Not necessarily. Tonnage capacity determines the maximum force available, not whether a part's geometry can be filled correctly in one die. A small, geometrically complex part run on an oversized press without the right die sequence can still suffer from folding or underfill defects. Tonnage and die design have to be matched together, not evaluated separately.
What's the difference between a blocker die and a finisher die?
A blocker (preform) die progressively redistributes metal from a simple billet shape toward the approximate geometry of the final part, without attempting to form fine detail. The finisher die then completes the precise shape, drawing on the pre-distributed metal volume the blocker stage already positioned. Complex geometries typically need both; simple geometries can often be formed in the finisher die alone.
How do I know if my part needs multi-die forging instead of single-die?
Parts with significant wall-thickness variation, deep ribs, non-symmetric branching, or fatigue-critical grain-flow requirements are strong candidates for multi-die forging. A supplier's simulation review — done before tooling is cut, not after defects appear — should confirm this rather than leaving it to assumption.
Can forging simulation software guarantee no defects before tooling is cut?
No responsible supplier should claim this. Simulation accuracy for solid-state aluminum forming typically runs in the 60–70% range for predicting die-fill and flow behavior; the remainder depends on engineer experience reviewing simulation output for risk areas the software may underrepresent. Treat 100% guarantees as a red flag rather than a reassurance.
What tonnage margin is standard when a supplier sizes a press for my part?
A commonly applied engineering guideline reserves 20–30% tonnage margin above the calculated peak forming load, to account for material variation, die wear, and press alignment tolerance. Ask your supplier for the calculated load per die stage, not just the press's rated capacity, to confirm this margin is actually being applied to your part.
What should I check during a supplier audit specifically related to press tonnage and die design?
Beyond tonnage capacity, ask about die-stage count and rationale, simulation software and its disclosed accuracy limits, first/mid/last-piece inspection methods, and the process for correcting die-cavity wear once detected. A supplier who can answer all of these with specifics — rather than general assurances — has a mature tonnage-and-die qualification process.
Conclusion
Tonnage capacity is necessary information, but it's the wrong first question. The question that actually predicts forging quality is whether the die sequence — single-die or multi-die — was matched to your part's geometry, validated by simulation before tooling was cut, and backed by a press class sized to the calculated load rather than whatever equipment happened to be available. Suppliers who can walk through that reasoning, with disclosed simulation limits and documented die-wear controls, are the ones worth shortlisting.
If you're evaluating a forging partner for a geometrically complex aluminum part, request a die-sequence and tonnage review before committing tooling budget — AFT's engineering team can walk through your part's specific requirements on a technical call.
For more technical guides like this one, see the AFT blog.