- Home
- Industries
- Aluminum Forging Bicycle Parts / Bike Parts
- Functional Teeth
Functional Teeth
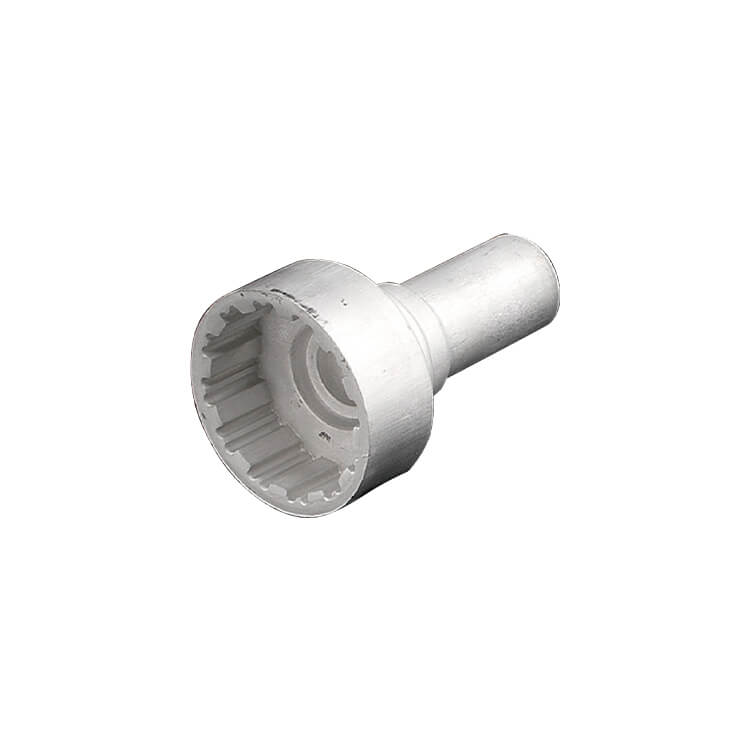
Forged Aluminum Bicycle Toothed Driver: Internally Toothed Cup and Shaft in One Piece
The forged aluminum bicycle toothed driver (functional teeth) is a toothed part for bicycle drivetrain or ratchet mechanisms. It consists of a cup with internal teeth and a cylindrical shaft extending from one end. Grooves are arranged around the inner wall of the cup to engage pawls, splines or mating teeth and transmit torque. Cup and shaft are formed in one piece, reducing fit errors between assembled parts.
Machining internal teeth requires dedicated operations such as gear shaping or broaching, which take time. Forging the tooth grooves to near-net shape first greatly shortens machining and keeps grain flow following the tooth form. Al Forge Tech (AFT) evaluates cold or hot forging by tooth accuracy and wall thickness, has an in-house broaching machine for finishing internal teeth, and inspects tooth form and concentricity with CMM and gauges.
Key Features
- Internally toothed cup and shaft formed in one piece
- Near-net forged teeth shorten shaping or broaching time
- In-house broaching for finishing internal teeth
- Tooth form and concentricity measured on CMM
Forged Aluminum Bicycle Toothed Driver Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Bicycle Parts |
| Application | Bicycle hub, ratchet and drivetrain toothed parts |
| Primary process | Hot or cold forging, selected by tooth accuracy and wall thickness (hot 600T–8,000T / cold 260T–2,500T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Bicycle Toothed Driver Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Cold forging: cold forming on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
Are the internal teeth forged or machined?
Both can be combined. Forging produces a near-net tooth profile to reduce machining; where tooth form and fit accuracy are critical, the teeth are finished to drawing tolerance by AFT's in-house broaching or CNC machining. AFT recommends the split between forming and machining at quotation based on tooth count, profile and tolerance grade, balancing die life and finished accuracy.
How can wear resistance of an aluminum toothed part be improved?
Aluminum teeth under repeated engagement must be protected against wear. Common practice is to select a suitable high-strength alloy, raise hardness by T6 heat treatment and add hard anodizing to form a hard oxide layer on the tooth faces. AFT offers both T6 heat treatment and hard anodizing; actual wear performance must be validated against the mating part's material and load conditions.
Can the Forged Aluminum Bicycle Toothed Driver be anodized or given other surface finishes?
Yes. Al Forge Tech offers anodizing (including hard anodizing), shot blasting, vibratory finishing, e-coating and painting, plus pickling and ultrasonic washing lines to clean parts after machining. Please note the finish type and film thickness on the drawing so machining allowances and cosmetic standards for the Forged Aluminum Bicycle Toothed Driver can be evaluated together.
How do you keep the Forged Aluminum Bicycle Toothed Driver consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Bicycle Toothed Driver stable across lots.
How are MOQ and lead time for the Forged Aluminum Bicycle Toothed Driver determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Bicycle Toothed Driver.
Request a Quote for the Forged Aluminum Bicycle Toothed Driver
Developing a new Forged Aluminum Bicycle Toothed Driver or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Bicycle Parts and our bicycle aluminum forging applications, or visit About Us for our equipment and certifications.