- Home
- Industries
- Aluminum Forging Moto Parts
- Triple Clamp
Triple Clamp
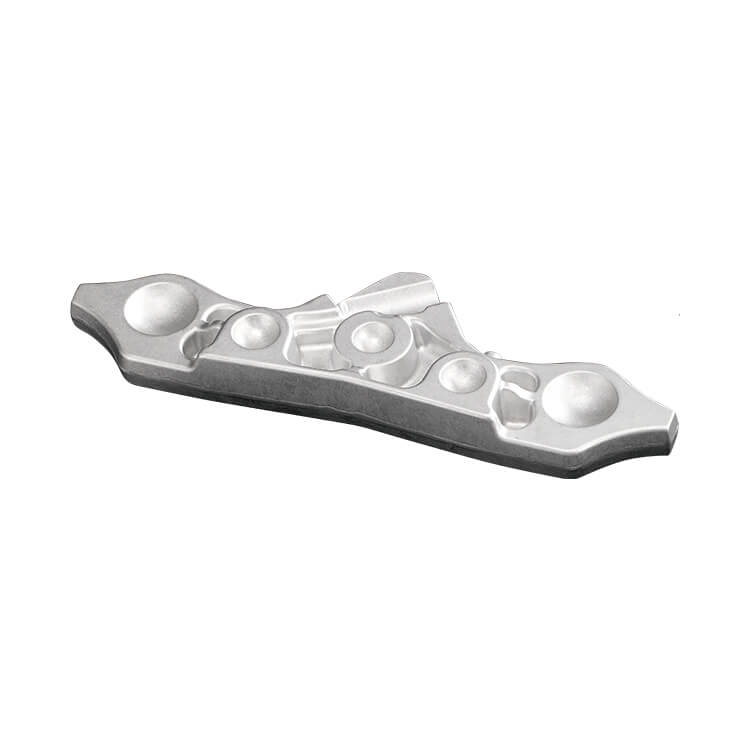
Forged Aluminum Motorcycle Triple Clamp (Multi-Boss): Long Crown with Multiple Mounting Points
This multi-boss forged aluminum motorcycle triple clamp is a longer fork crown whose body carries multiple round bosses and ribs. Beyond the fork bores at each end and the central steerer bore, the bosses can serve as mounting points for instruments, steering stops, cable guides or handlebar mounts. The multi-boss design combines structure with accessory integration.
The more bosses there are, the more complex material distribution becomes during forging. Al Forge Tech (AFT) confirms fill of every boss with QForm simulation, closed-die hot forges the clamp and completes T6 heat treatment in-house, then machines all bores and boss threads on 4.5-axis CNC to reduce re-clamping, verifying the position of each mounting point on CMM.
Key Features
- Multiple round bosses integrate accessory mounting points
- Ribbed long body for stiffness
- 4.5-axis CNC multi-face machining reduces re-clamping
- Position of every mounting point measured on CMM
Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Moto Parts |
| Application | Fork crowns for motorcycles and powersport vehicles that integrate accessory mounts |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Per customer specification; heavy-motorcycle parts produced in grades such as 6061-T6, 2014-T6 and 7075-T6 |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
What can the bosses on the triple clamp be used for?
Depending on the model, the bosses can be machined as threaded mounts for instrument or windscreen brackets, steering stops, cable or hose guides, or handlebar mounts. Integrating these points into the clamp forging eliminates extra brackets and welded parts, simplifies the front-end structure and reduces assembly time.
How is complete fill of every boss ensured?
More bosses mean metal must flow to more scattered locations, and local shortage can leave a boss incompletely filled. AFT simulates the fill sequence of each boss with QForm at the die design stage, adjusts billet shape and flash design, checks first, middle and last pieces in every lot, and measures boss position and height on CMM.
Is heat treatment for the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) done in-house?
Yes. Al Forge Tech operates 8 T4 solution treatment units and 7 T6 artificial aging units on site, so the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) can be solution treated, quenched and aged in the same facility before machining and inspection. Keeping heat treatment in-house removes inter-plant transport, reduces lead-time risk and keeps lot traceability within one quality system. Parameters are set according to the alloy grade and your specification.
How are MOQ and lead time for the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss).
How do you keep the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) stable across lots.
Request a Quote for the Forged Aluminum Motorcycle Triple Clamp (Multi-Boss)
Developing a new Forged Aluminum Motorcycle Triple Clamp (Multi-Boss) or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Moto Parts and our motorcycle aluminum forging applications, or visit About Us for our equipment and certifications.