Seat Post
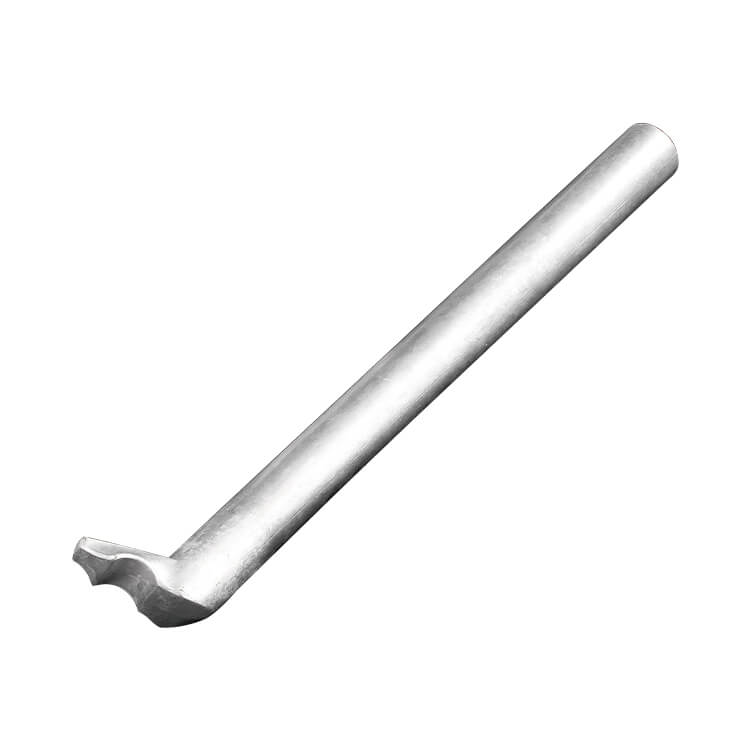
Forged Aluminum Bicycle Seat Post: Shaft and Saddle Clamp Head in One Piece
The forged aluminum bicycle seat post connects the saddle to the frame. It is a long slender tube with a bent saddle clamp head at the top for mounting the saddle rail clamp. A one-piece seat post forms the shaft and clamp head together, with no welded or bolted-on head, giving a simple, light structure.
The bent clamp head carries the bending load from the rider's weight and is the most heavily stressed area of the post. Al Forge Tech (AFT) forges the head so grain flow turns continuously from shaft into head, avoiding the heat-affected weakening of a welded head. After heat treatment, the clamp bore, threads and shaft diameter are machined, and anodizing or shot blasting can be applied for appearance and corrosion resistance.
Key Features
- Shaft and saddle clamp head formed in one piece, no weld
- Continuous grain flow through the bent head under bending load
- Clamp bore, threads and shaft diameter machined
- Anodized or shot-blasted finish
Forged Aluminum Bicycle Seat Post Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Bicycle Parts |
| Application | Seat posts for bicycles and e-bikes |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Bicycle Seat Post Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
How does a one-piece seat post differ from one with a welded head?
A welded-head post has the clamp head welded to the shaft, and the weld and heat-affected zone are usually weaker than the base metal, right where bending load is highest. A one-piece post is formed from a single piece of material with continuous grain flow through the bend and no weld, giving a simpler structure and eliminating welding and straightening steps.
Can the seat post diameter be customized to the frame?
Yes. Diameter, length, clamp head angle and setback can all be developed to the brand's drawing. AFT evaluates the forming method by shaft length and wall thickness, finish-machines the diameter after heat treatment and checks diameter tolerance and straightness with CMM and gauges to ensure the fit with the frame's seat tube.
How does a forged aluminum Forged Aluminum Bicycle Seat Post compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Bicycle Seat Post under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
How do you keep the Forged Aluminum Bicycle Seat Post consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Bicycle Seat Post stable across lots.
Can you assess forging feasibility while the Forged Aluminum Bicycle Seat Post is still in design?
Yes. Al Forge Tech works mainly as an OEM supplier, and our engineers can give design-for-manufacturability (DFM) feedback at the concept or drawing stage, such as adjusting thin ribs, abrupt section changes or draft angles to avoid laps and underfill. QForm simulation predicts metal flow early, and the results are cross-checked against our die design experience.
Request a Quote for the Forged Aluminum Bicycle Seat Post
Developing a new Forged Aluminum Bicycle Seat Post or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Bicycle Parts and our bicycle aluminum forging applications, or visit About Us for our equipment and certifications.