- Home
- Industries
- Aluminum Forging Vehicle Parts
- Rear Supporting Bracket
Rear Supporting Bracket
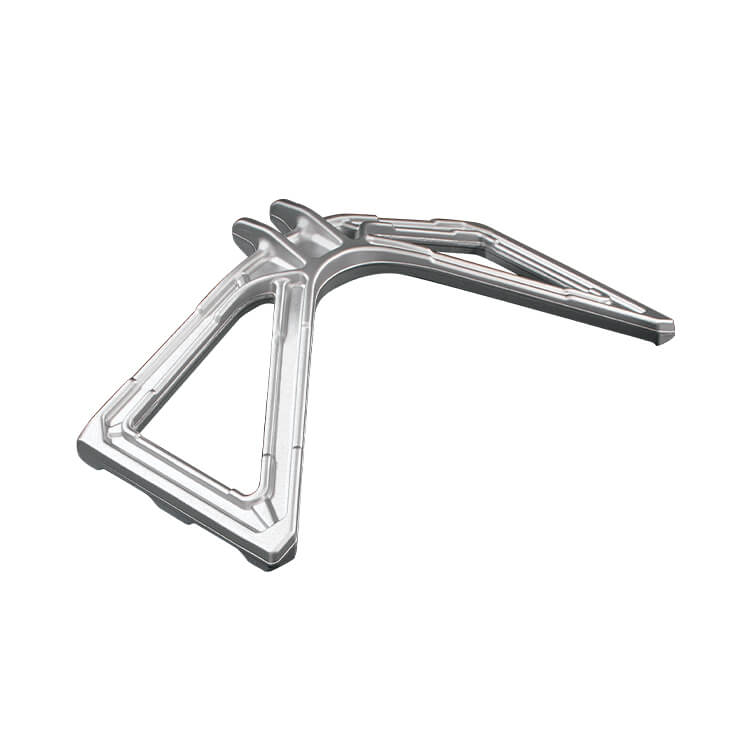
Forged Aluminum Rear Supporting Bracket: Snowmobile Rear Suspension Bracket
The forged aluminum rear supporting bracket is a structural bracket in a snowmobile's rear suspension. It is a truss made of a triangular frame and an extended arm, with an open frame to save weight and mounting bosses at each end that connect to the rear suspension rails, shock absorber and chassis. The bracket is forged in one piece, replacing a multi-part welded assembly.
Snowmobiles run in cold, high-impact conditions, so the rear bracket must carry repeated impacts and torsional loads from the snow surface. Al Forge Tech (AFT) closed-die hot forges the bracket so grain flow runs continuously along the frame members, avoiding the heat-affected weakening at welded joints, and finishes mounting holes and mating faces after in-house T6 heat treatment and CNC machining.
Key Features
- Triangular truss forged in one piece, replacing welded assemblies
- Open-frame design balances rigidity and weight
- All mounting points CNC-machined and CMM-checked
- Suited to cold, high-impact snowmobile rear suspension
Forged Aluminum Rear Supporting Bracket Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Vehicle Parts |
| Application | Snowmobile rear suspension systems, structural brackets for powersport vehicles |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Per customer specification; 6xxx alloys common for chassis and suspension parts (e.g. 6061, 6082, 6110), 7xxx evaluated for higher strength |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant line; tensile and fatigue testing available |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Rear Supporting Bracket Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
Why replace a welded snowmobile bracket with a forging?
A welded bracket is assembled from several profiles or tubes, and the weld and heat-affected zone are usually weaker than the base metal, making them likely fatigue-crack initiation sites under repeated impact. A forged bracket is a single piece without welded joints, with grain flow continuous along the members. It also eliminates assembly steps and fixtures and makes dimensional consistency easier to hold in production.
How are distortion and hole accuracy controlled on a large frame forging?
Frame forgings can distort during quenching because of uneven sections. AFT balances member sections during die and process design, straightens after heat treatment, and CNC-machines the mounting holes afterward so heat-treatment distortion does not affect hole positions. Hole positions and flatness are then measured on Zeiss CMM.
How does a forged aluminum Forged Aluminum Rear Supporting Bracket compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Rear Supporting Bracket under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
How do you keep the Forged Aluminum Rear Supporting Bracket consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Rear Supporting Bracket stable across lots.
How are MOQ and lead time for the Forged Aluminum Rear Supporting Bracket determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Rear Supporting Bracket.
Request a Quote for the Forged Aluminum Rear Supporting Bracket
Developing a new Forged Aluminum Rear Supporting Bracket or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: aft@aft-forge.com.tw
To compare similar parts, browse Aluminum Forging Vehicle Parts and our automotive aluminum forging applications, or visit About Us for our equipment and certifications.